Ring

Six-Axis Robot Integration for Injection Molding Plate Handling — MetalPlast

ByMateja Cveticanin
Process Automation Engineering
Serbia
4 minutes
Six-Axis Robot Integration for Injection Molding Plate Handling — MetalPlast - Image 1
Six-Axis Robot Integration for Injection Molding Plate Handling — MetalPlast - Image 2
Six-Axis Robot Integration for Injection Molding Plate Handling — MetalPlast - Image 3
Six-Axis Robot Integration for Injection Molding Plate Handling — MetalPlast - Image 4
Six-Axis Robot Integration for Injection Molding Plate Handling — MetalPlast - Image 5

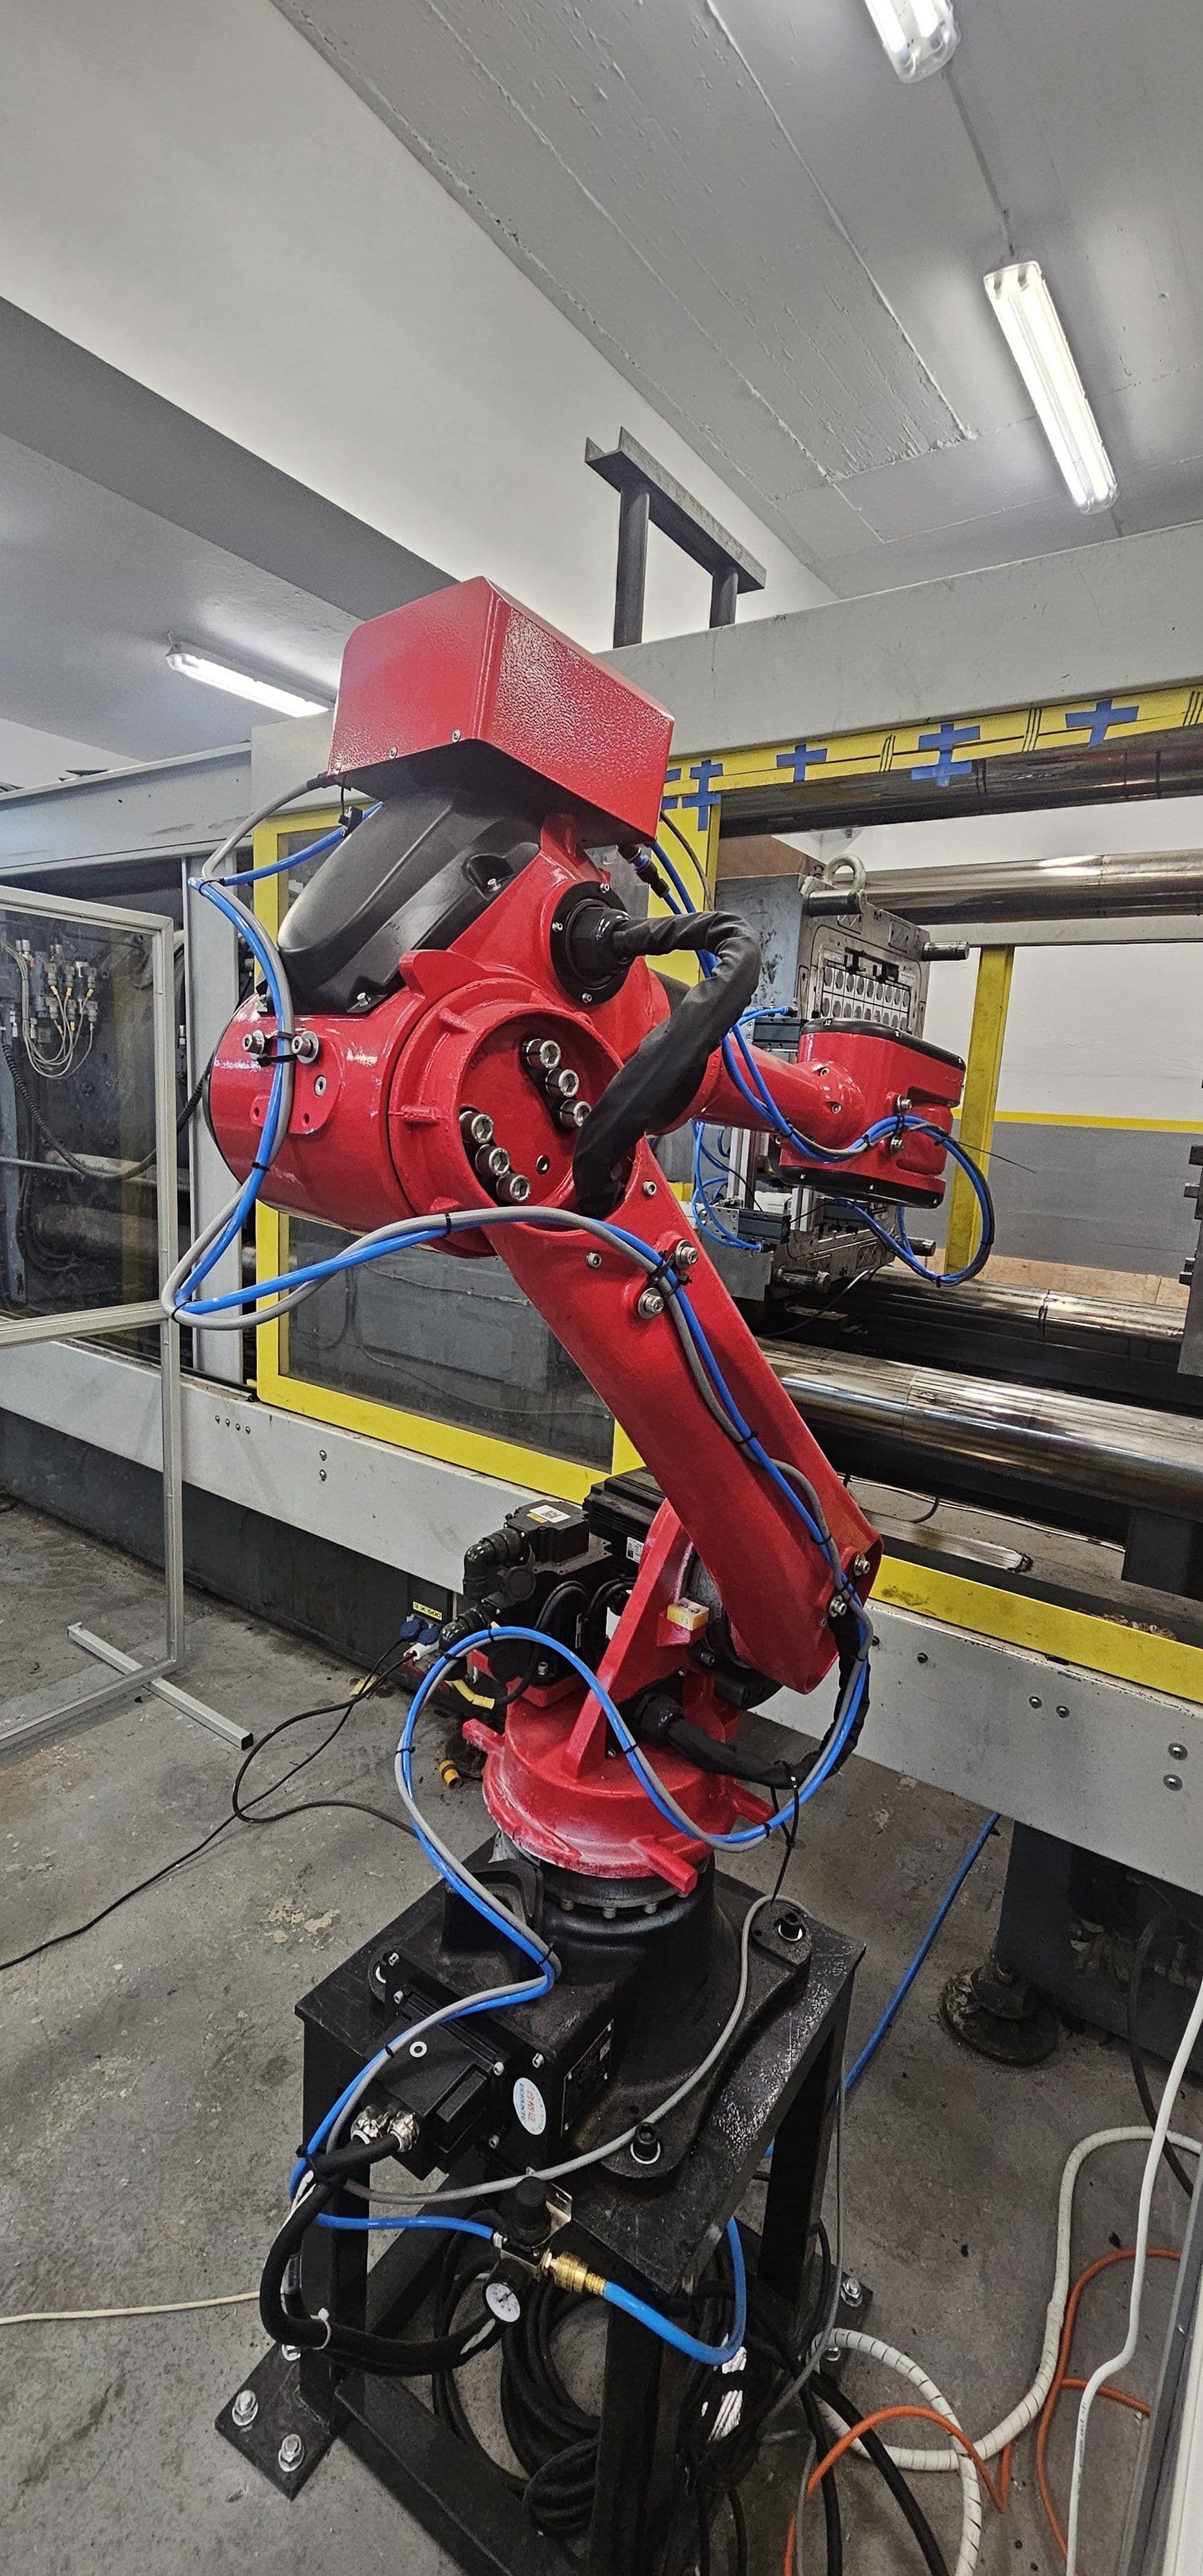
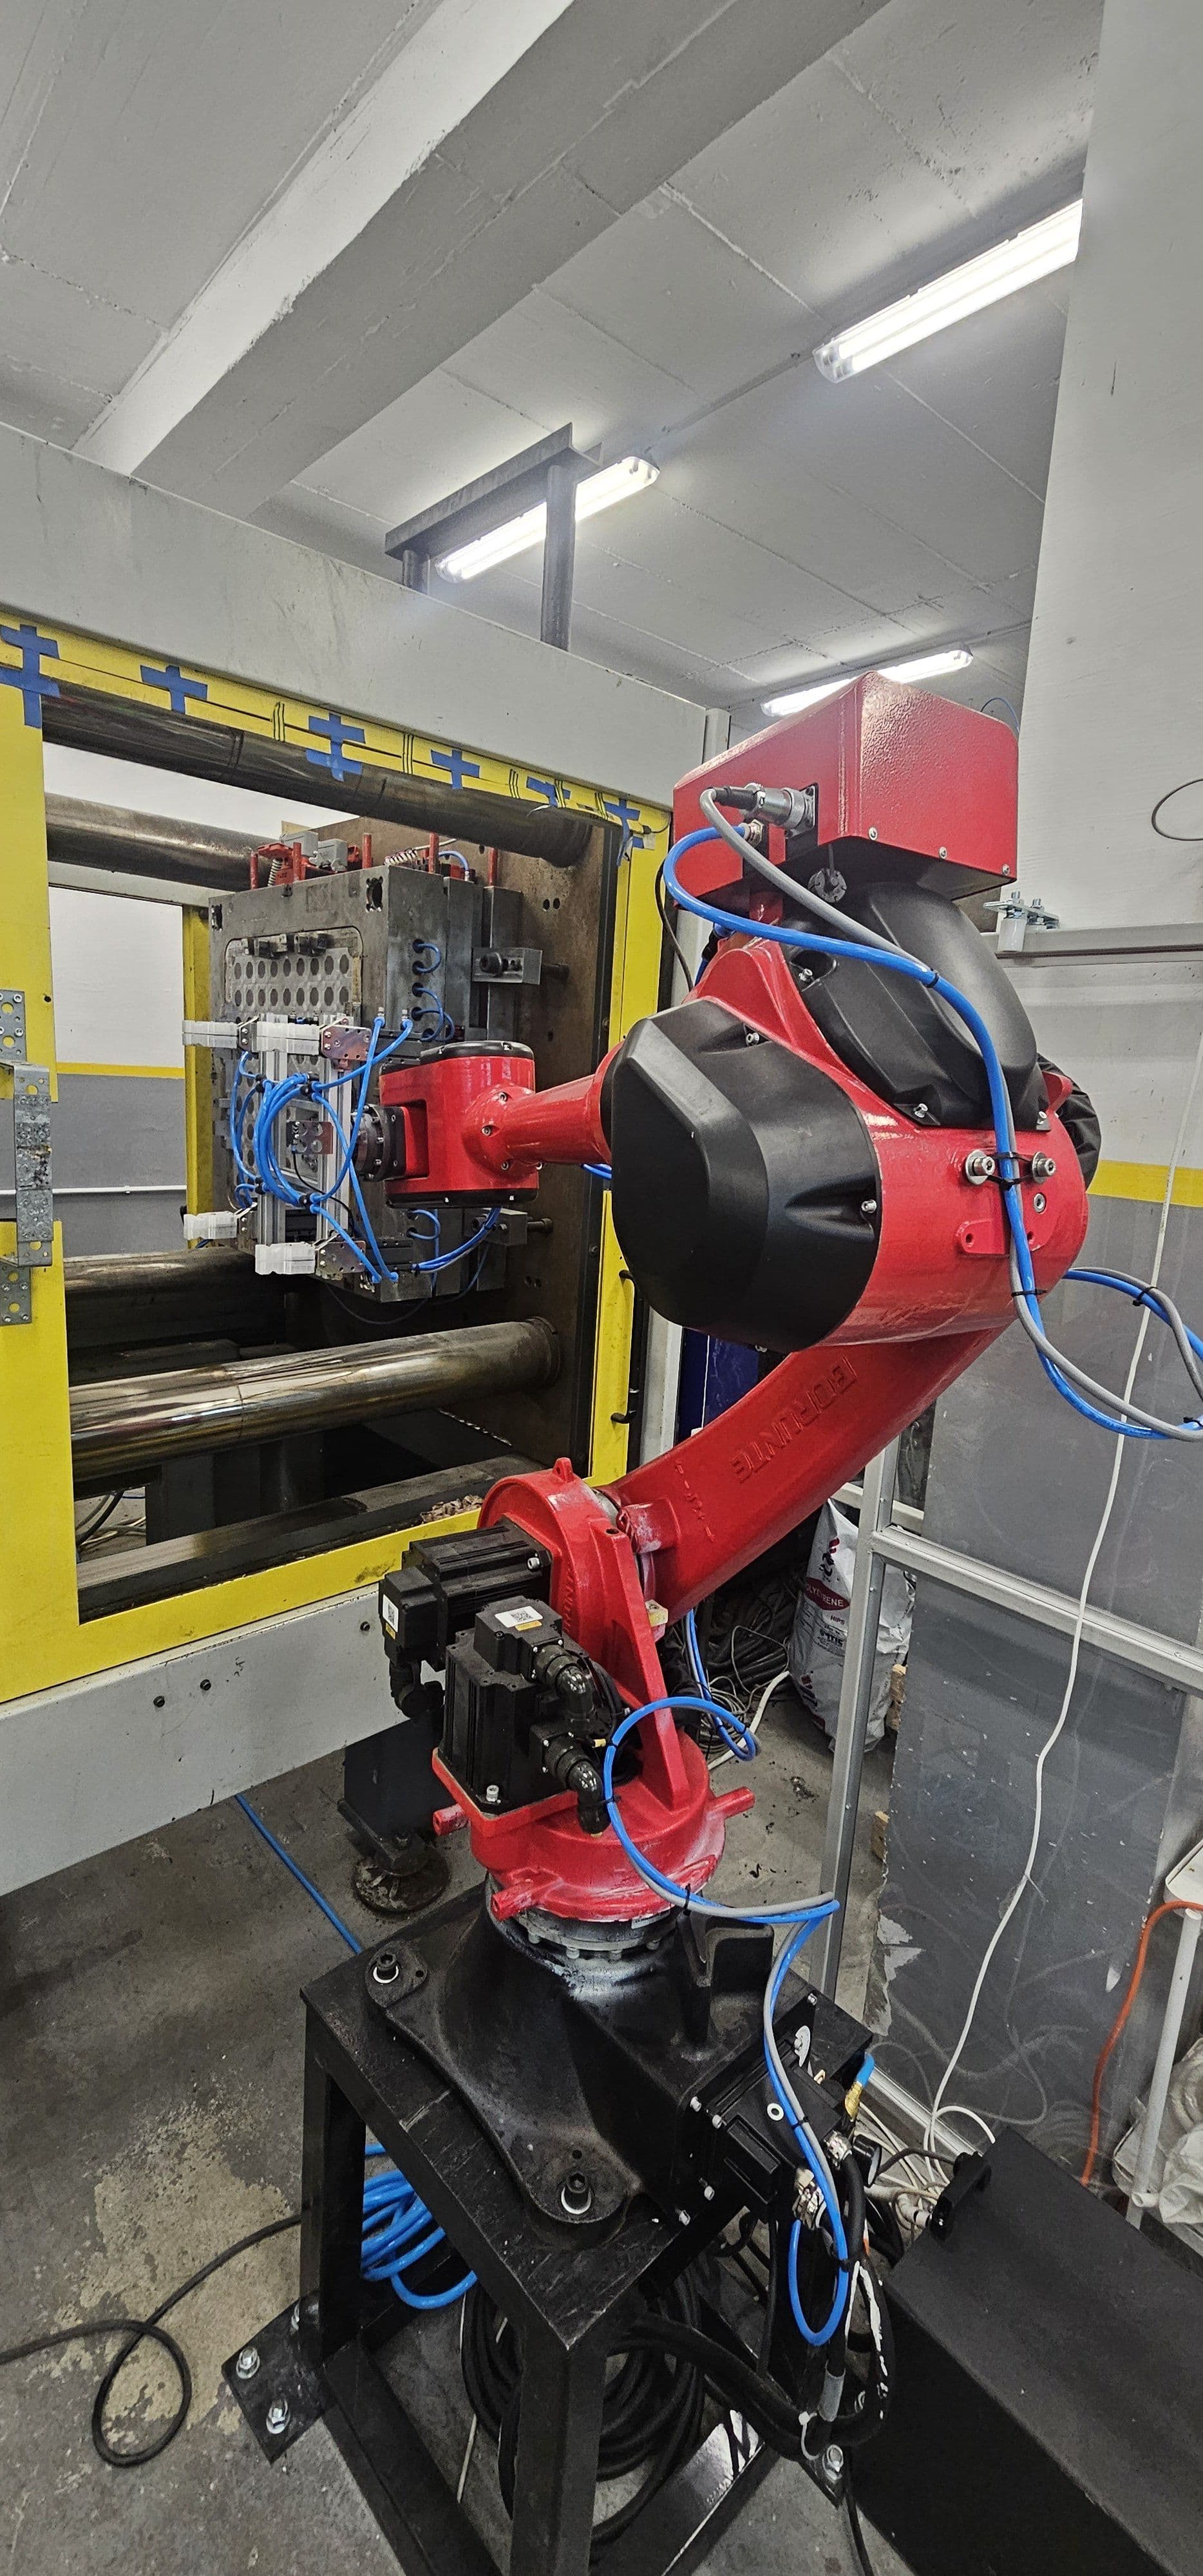
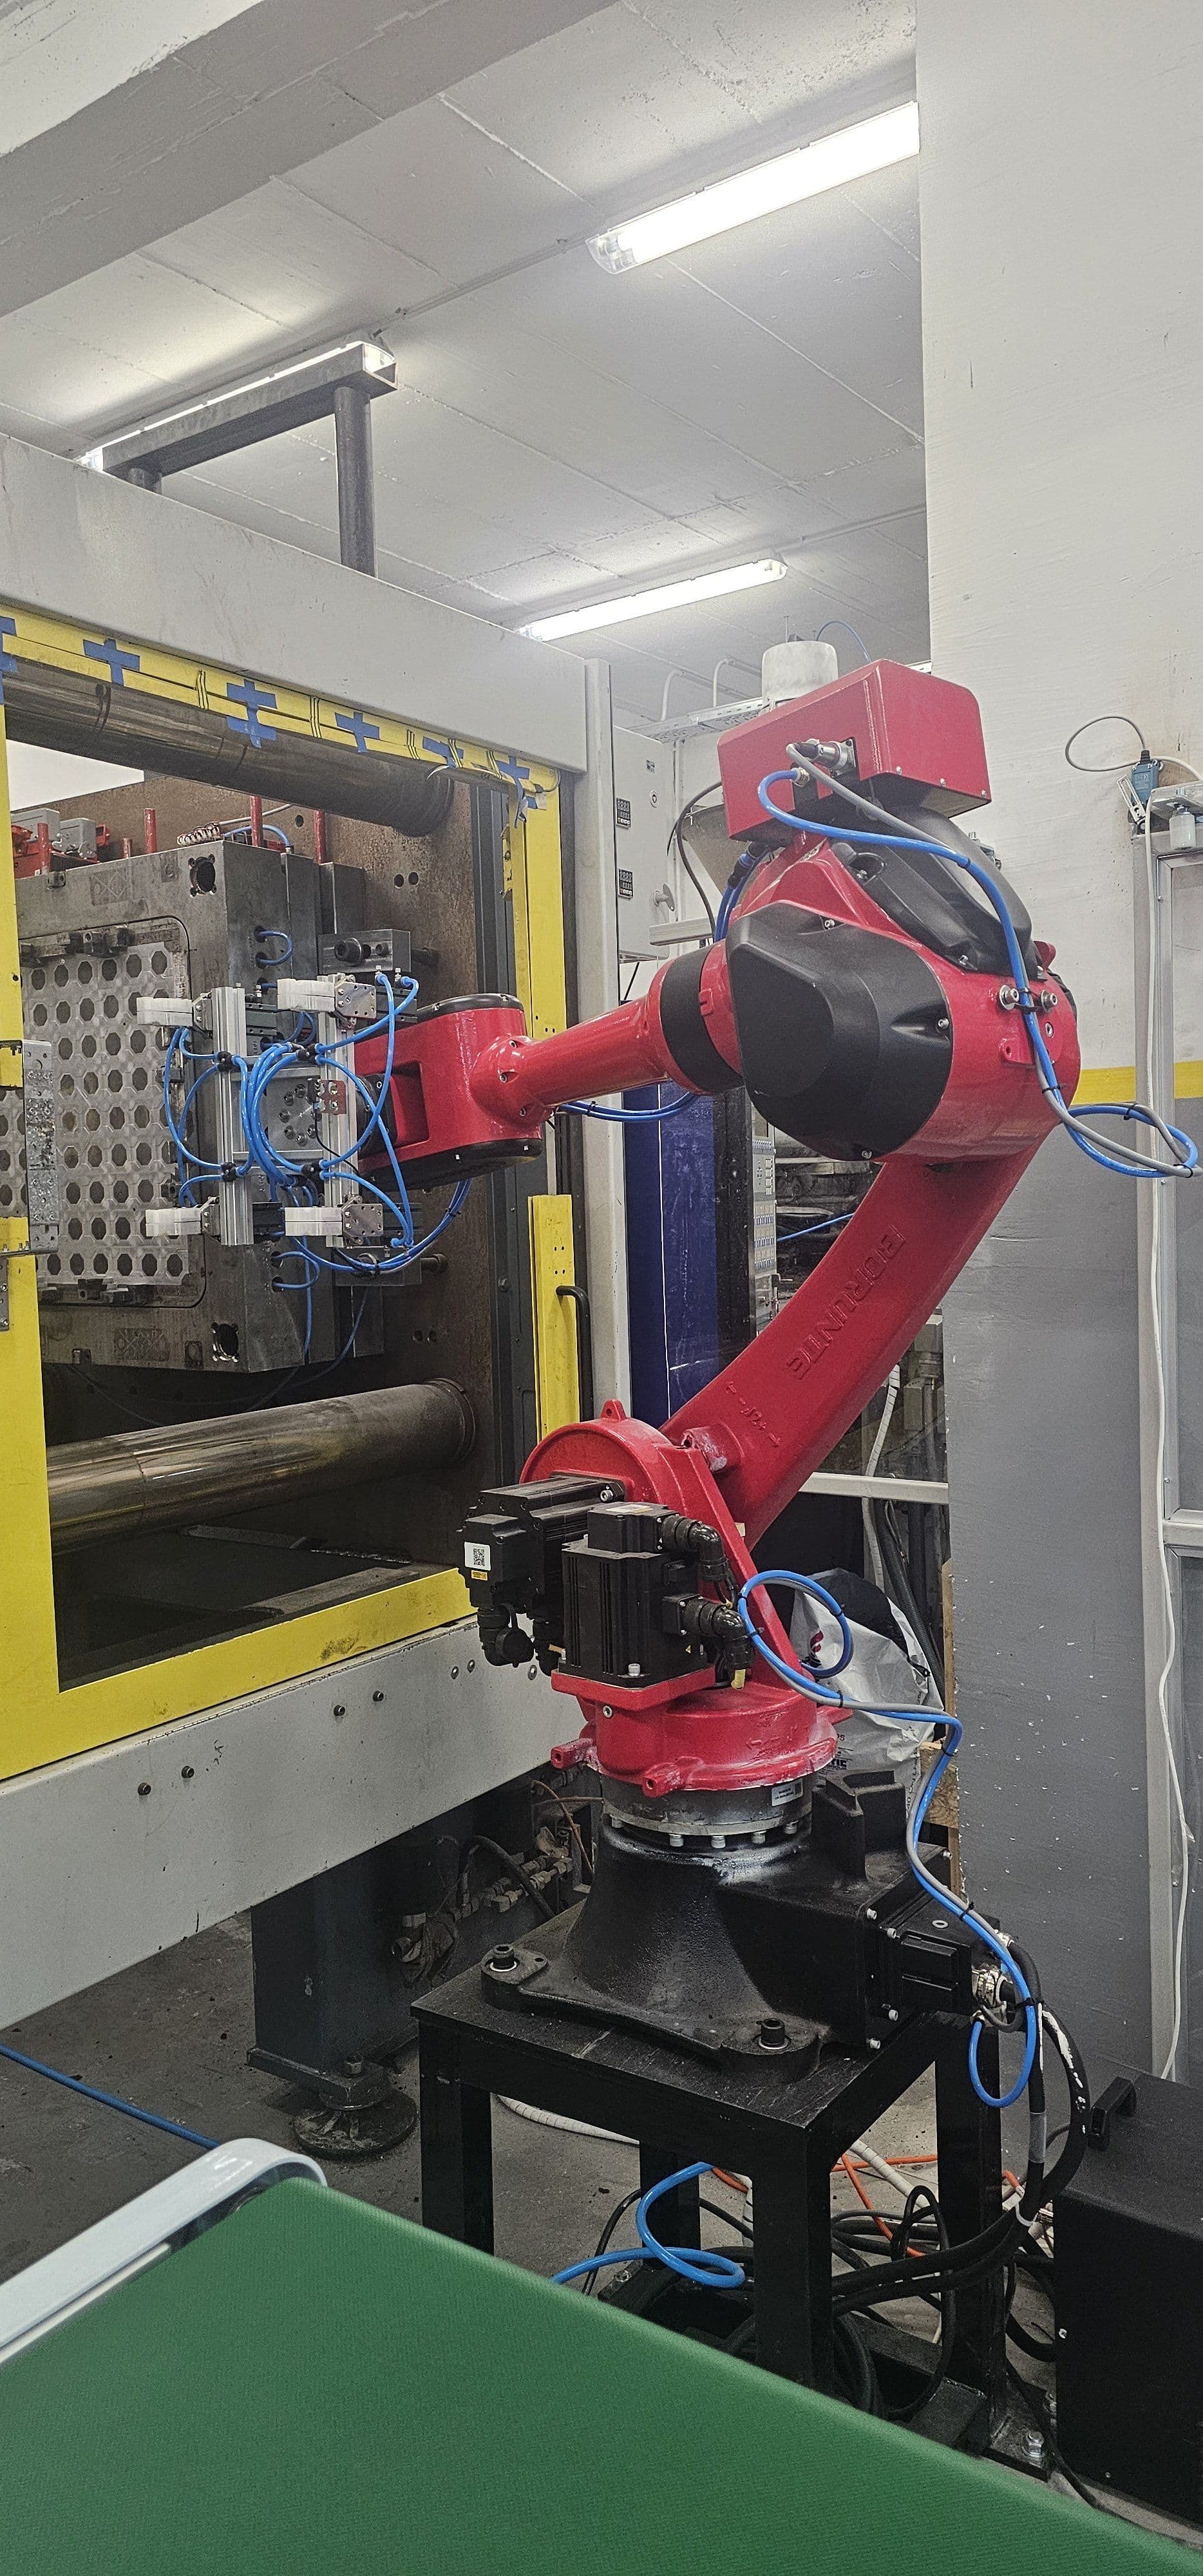
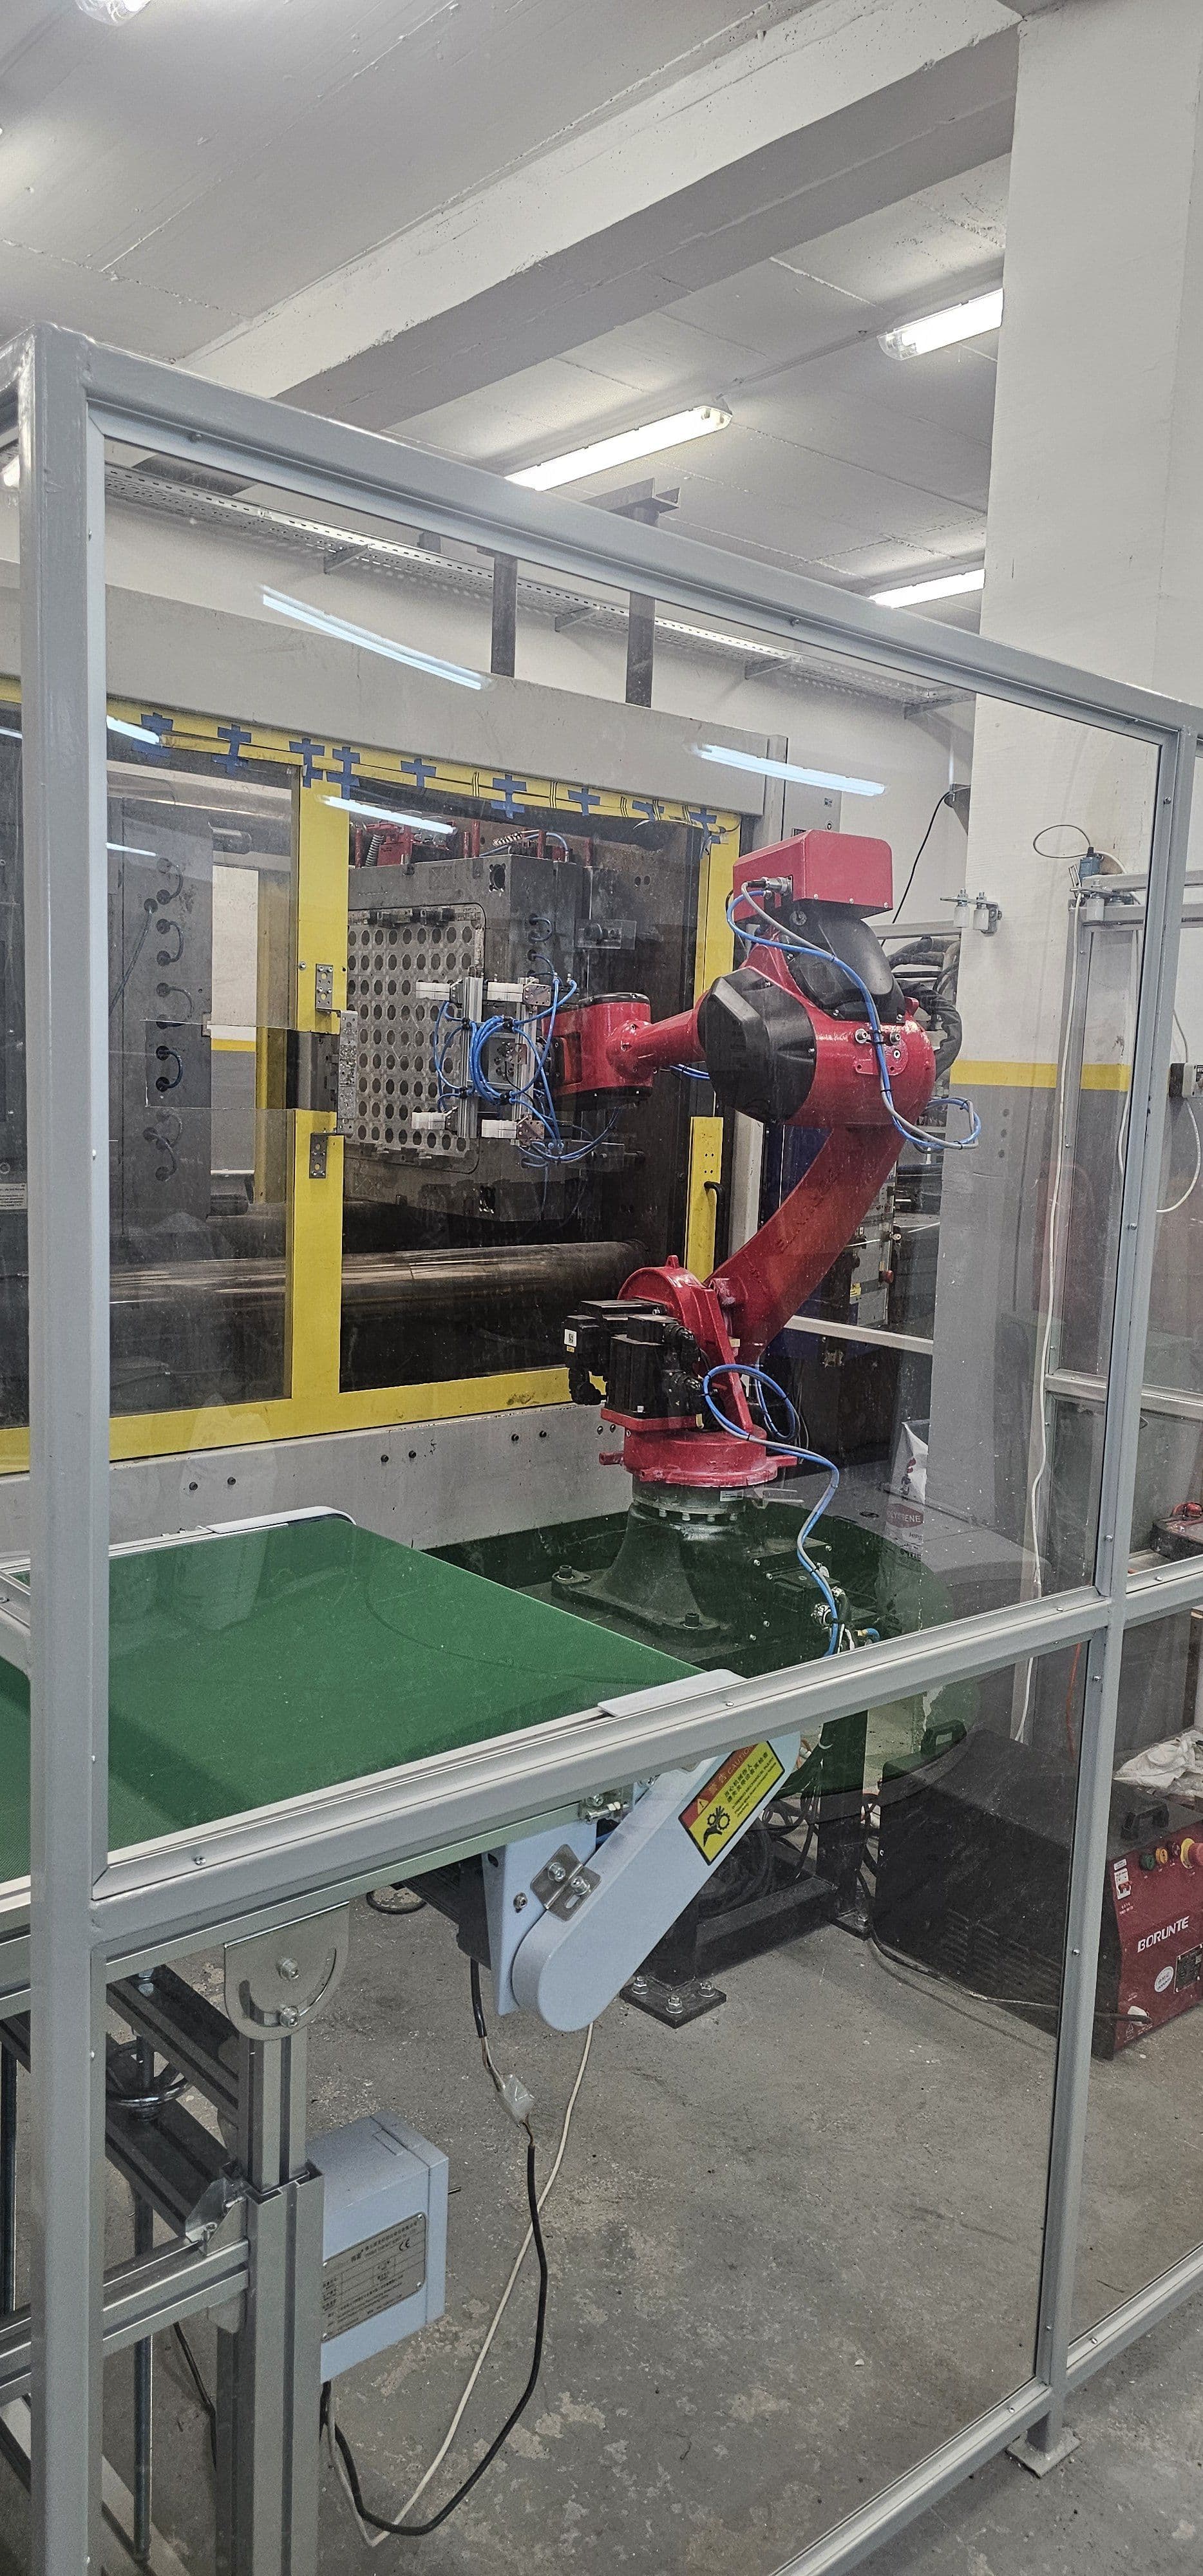
Triton Engineering — with Sweden Engineering Partner (SE-EP) — integrated a client-owned six-axis robot with an injection molding press at MetalPlast. Automated plate pickup, two-plate stacking and conveyor indexing for unattended production.

THE CHALLENGE

Side-Entry Access, EUROMAP Sync, and Reliable Vacuum Pickup

MetalPlast operates a plastic injection molding press producing perforated plates around 500×500 mm. The existing manual pickup workflow created a bottleneck at the press and ruled out continuous unattended operation. SE-EP, the Swedish integration partner on this project, brought in Triton Engineering to design and commission the automation cell around the client-owned six-axis robot.

  • Restricted overhead clearance ruled out a top-entry approach — the robot had to enter and exit the open mold area from the side on every cycle.
  • Cycle synchronization with the press demanded an industrial EUROMAP 12 interface — generic I/O wiring would not have satisfied operational safety or repeatability.
  • Perforated plates require a vacuum gripper with redundant zones — a single vacuum loss must not drop a part during high-speed extraction.
  • Two plates per cycle had to be reliably stacked and indexed on the downstream conveyor without operator intervention.
THE SOLUTION

Side-Entry Vacuum EOAT and EUROMAP 12 Synchronization

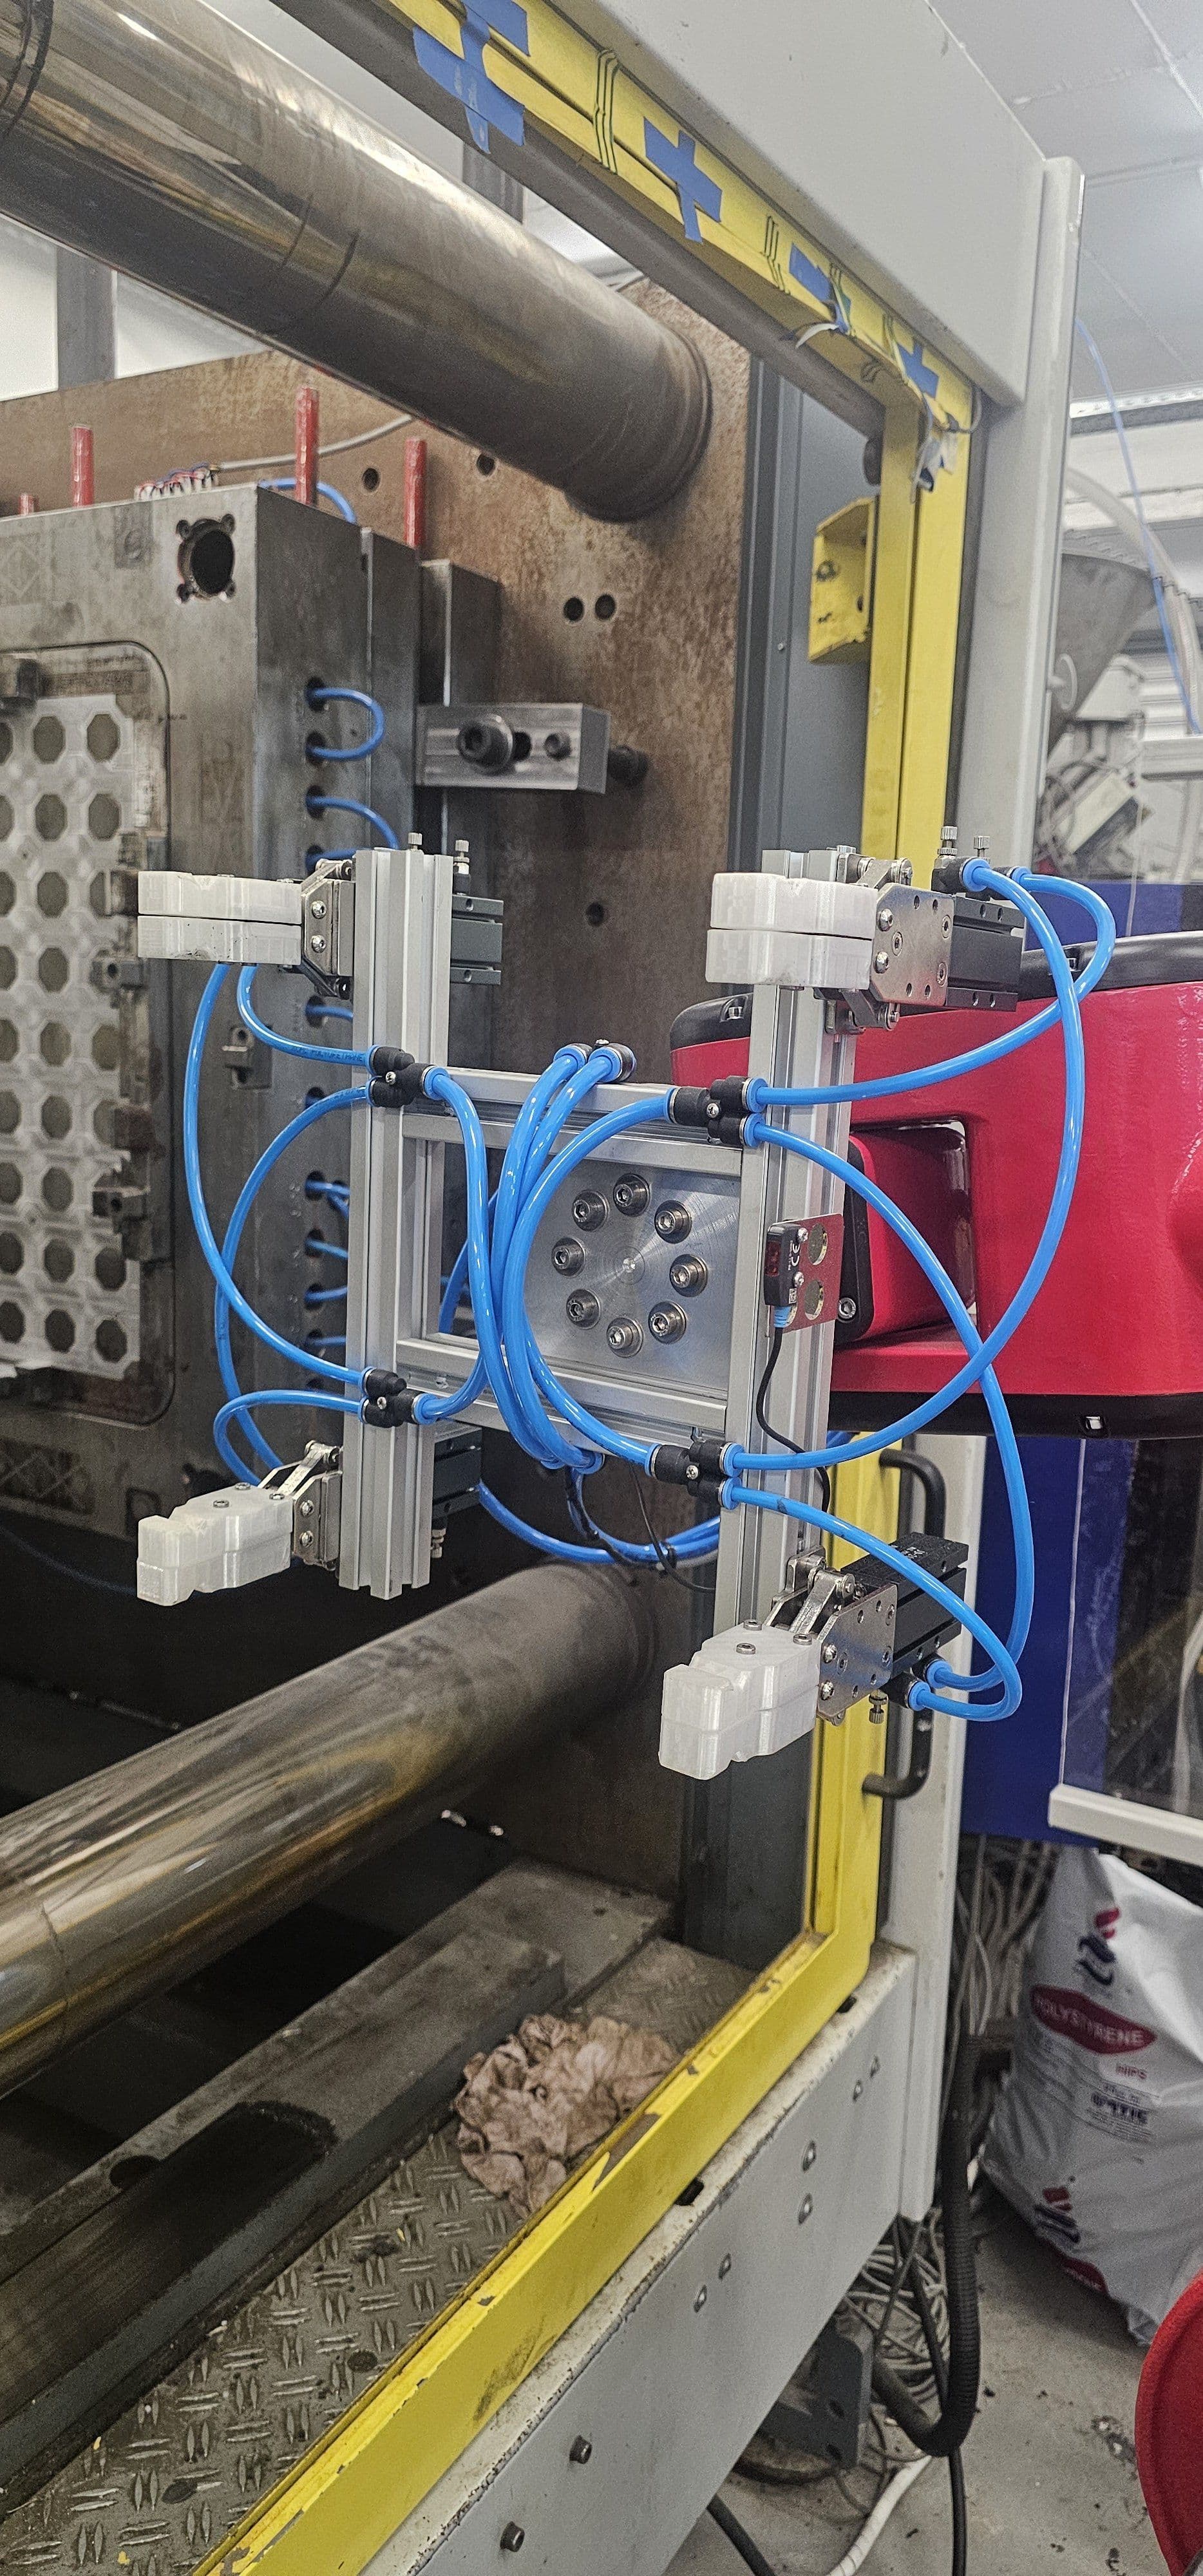
Triton delivered a two-zone vacuum end-of-arm tool, the EUROMAP 12 interface cable, complete robot programming and on-site commissioning. The result: hands-off pickup-and-stack cycles, driven by the press's own mold-open signal.

  • Two-Zone Vacuum EOAT: Custom end-of-arm tool with two independently controlled vacuum zones — each with its own ejector, valves, and confirmation sensing, so plates with holes are held securely throughout extraction.
  • EUROMAP 12 Interface: Standardized industrial cable links the robot to the injection press for mold-open and part-out handshake — no custom electronics or proprietary middleware in the signal path.
  • Side-Entry Trajectories: Robot motion paths were programmed to enter and exit the mold area through the narrow lateral opening with minimum dwell — preserving press takt time.
  • Pickup Confirmation Logic: Vacuum is verified at both zones before the robot retracts from the mold area — if confirmation fails, the cycle holds and the operator is alerted, with no risk of dropped parts inside the tool.
  • Two-Plate Stacking Sequence: Each cycle places two plates onto an indexing conveyor that advances one position downstream — stable, hands-off material flow toward the next process step.
  • On-Site Commissioning: Triton's engineering team commissioned the cell at MetalPlast, ran a live production batch, tuned vacuum and motion parameters, and trained the press operators.
PRODUCTS USED

Equipment & Systems

  • Two-zone vacuum EOAT: Ejectors, suction cups, valves, manifolds, hoses, fittings, gauges and the aluminum mounting frame — engineered for ~500×500 mm perforated plates.
  • EUROMAP 12 ↔ EUROMAP 67 cable: 5 m industrial interface cable connecting the client robot to the injection molding press for synchronized cycle operation.
  • Robot programming: Side-entry trajectories, pickup and stacking sequences, vacuum-zone control logic, and safety-zone definitions on the client-owned six-axis robot.
  • EUROMAP handshake & sequences: Mold-open, part-out and ready signals coordinated between robot and press using standardized industrial messaging.
  • On-site commissioning (SAT): Live production run on the client floor, parameter tuning, operator training, and signed acceptance protocol.

Subsystem Suppliers & Integration Partner::

  • INDAS vacuum components (ejectors, suction cups, valves, manifolds, gauges)
  • EUROMAP 12 / EUROMAP 67 industrial interface cable (5 m)
  • Pneumatic hoses, fittings, and air preparation hardware
  • Aluminum profile frame for the EOAT structure
  • Client-owned six-axis articulated robot (integration only — not supplied by Triton)
  • SE-EP — Sweden Engineering Partner (project coordination and Nordic-market liaison)
RESULTS

MetalPlast's injection press now runs an automated pickup-and-stack cycle directly from the open mold. Operator workload at the press dropped to monitoring only, takt time is repeatable, and the line is ready for continuous unattended shifts.

Injection Molding Robot Automation — MetalPlast Case Study | Triton Solutions Blog